
6 Best Welding Rods For Boat Hull Maintenance For Repairs
Keep your vessel seaworthy with our top 6 best welding rods for boat hull maintenance. Click here to choose the right materials for your next repair project.
A hull breach or a failing weld on a boat is not merely an inconvenience; it is a critical threat to the structural integrity of a mobile home that happens to float. Maintaining that steel or aluminum skin requires the right consumables, as standard hardware store rods often lack the metallurgical precision needed for marine environments. Choosing the correct welding rod ensures that repairs hold up against the constant vibration, salt spray, and thermal cycling inherent to life on the water.
Disclosure: As an Amazon Associate, this site earns from qualifying purchases. Thank you!
Lincoln Electric Fleetweld 37: Best All-Purpose Rod
The Lincoln Electric Fleetweld 37 is the industry standard for light-to-medium steel repairs on a boat hull. Its smooth arc and easy slag removal make it exceptionally forgiving for vertical or overhead welding, which is frequently required when patching hull plates while the boat is in the water or dry-docked.
This rod excels at welding thin-gauge steel where burn-through is a constant risk. Because it runs well on both AC and DC machines, it is the most versatile option for those who might be working with limited power supplies in a marina or remote dock setting.
If a project involves basic steel maintenance—like repairing an engine mount or patching non-structural plating—this rod is the correct choice. It is not designed for high-stress structural joints, so avoid using it on primary keel or frame reinforcements.
Hobart 418 (E7018): Best for Structural Repairs
When the structural integrity of a hull is compromised, the Hobart 418 provides the necessary strength to return the vessel to service safely. As an E7018 rod, it offers high-tensile strength and superior crack resistance, which are essential for welds that will be subjected to the constant pounding of waves and hull flexing.
This rod produces a high-quality, ductile weld that can withstand significant impact and vibration. Because it is a low-hydrogen electrode, it creates a clean joint that is far less prone to internal porosity than standard mild steel rods.
This is the rod to reach for when repairing cracked hull frames, engine beds, or load-bearing bulkheads. Do not attempt to use this for thin, cosmetic skin repairs, as the higher heat input required can easily distort thinner sheet metal.
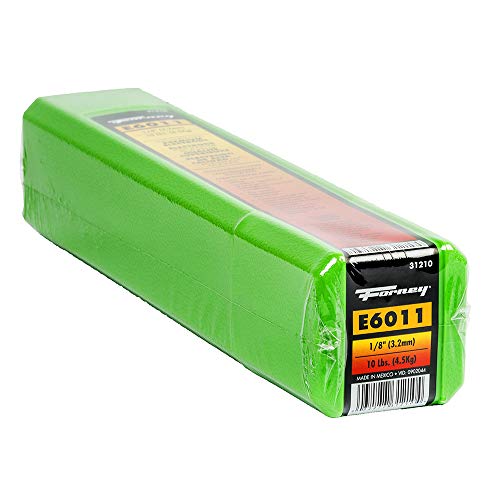
Forney E6011: Best for Rusty or Painted Surfaces
Boats often require emergency repairs where the base metal is less than pristine. The Forney E6011 is designed to dig deep and penetrate through light rust, scale, or residual paint, making it the superior choice for field repairs where thorough surface preparation is difficult.
The fast-freezing slag allows for excellent control, even if the fit-up of a patch panel is imperfect. This capability is vital for DIY repairs where the hull may have irregular shapes or gaps that require a “fill-in” welding approach.
It is best to reserve this rod for dirty, outdoor repair scenarios where surface cleaning is restricted. For clean, new metal repairs, look elsewhere, as the E6011 leaves a rougher bead profile that requires significantly more grinding and finishing work.
Blue Demon 316L-16: Best for Stainless Fittings
Stainless steel requires specific chemistry to prevent “weld decay” and corrosion in saltwater environments. The Blue Demon 316L-16 is specifically formulated to maintain the corrosion resistance of 316-grade stainless, ensuring that repairs to railings, swim platforms, or thru-hull fittings do not begin to rust immediately.
This rod offers a stable arc and low spatter, which is essential when working near delicate boat finishes or fiberglass. A clean weld means less time spent grinding away splatter and polishing the stainless to restore its protective finish.
If a project involves welding stainless steel components exposed to the marine atmosphere, this is the only logical choice. It is not suitable for carbon steel, so ensure the base metal is verified as stainless before attempting a weld.
ESAB Atom Arc 7018: Best Low-Hydrogen Option
The ESAB Atom Arc 7018 is the benchmark for low-hydrogen performance, providing a stable, reliable weld for critical hull junctions. Low-hydrogen rods are essential for thick-plate welding on vessels, as they drastically reduce the risk of hydrogen-induced cracking in the weld bead.
This rod handles exceptionally well in all positions, which is often a challenge when working in the cramped, awkward compartments common in boat interiors. The consistent bead profile it produces makes it easier to inspect welds for quality—a necessity when dealing with marine safety standards.
This is the preferred rod for professional-grade repairs on heavy-gauge steel hulls. If a repair involves thick sections of steel that take the brunt of wave energy, do not compromise with a cheaper general-purpose rod; use the Atom Arc.
U.S. Forge Aluminum Rod: Best for Aluminum Hulls
Welding aluminum is a specialized task that requires different equipment and consumables compared to steel. The U.S. Forge Aluminum rod is formulated for repairing cast and wrought aluminum parts, making it a viable option for quick, non-critical repairs on aluminum hull sections or outboard brackets.
Working with aluminum rods requires a different technique, as the material conducts heat rapidly and can melt unexpectedly. This rod is best suited for those with some experience in arc welding, as it demands a steady hand and precise travel speed to prevent the metal from collapsing.
This is an excellent tool for field-repairing aluminum hardware or small cracks in non-load-bearing areas. It is not recommended for full hull-plate replacements, which typically require TIG or MIG welding processes for structural integrity.
Choosing the Right Rod for Your Hull Material
The most common mistake when repairing a hull is mismatching the filler material to the base metal. Always identify the grade of steel or aluminum—using a magnet or checking manufacturer documentation—before selecting a rod.
- Carbon Steel: Use E6011 for repairs with heavy rust and E7018 for structural integrity.
- Stainless Steel: Always use a 316L rod to ensure the weld remains as corrosion-resistant as the surrounding metal.
- Aluminum: Use specialized aluminum-specific rods for minor repairs, but be prepared for high thermal conductivity.
When in doubt, choose the stronger rod, such as an E7018, for load-bearing areas. Never use stainless rods on mild steel, as this will lead to galvanic corrosion, eventually eating away the steel around the weld.
Critical Safety for Welding On Your Boat
Welding on a boat introduces unique hazards, primarily due to the proximity of fuel lines, electrical wiring, and fiberglass. Always remove any fuel sources from the immediate area and ensure a fire extinguisher is within reach at all times.
Because boat hulls can act as large heat sinks or, conversely, trap heat in confined spaces, ventilation is vital. Arc rays can also reflect off of metal walls, so ensure all exposed skin is covered to prevent severe “sunburn” from the welding arc.
Finally, disconnect the boat’s main battery bank before striking an arc. An accidental grounding through the boat’s electrical system can fry expensive navigational equipment, batteries, and bilge pump sensors in a fraction of a second.
How to Properly Store Your Welding Rods
Welding rods, especially low-hydrogen types like E7018, are highly susceptible to moisture absorption. Once the flux coating absorbs water, the rod will cause porosity in the weld, leading to weak spots that can fail under stress at sea.
Keep all welding rods in a sealed, airtight container, preferably equipped with a desiccant pack. For those living in humid climates or near the coast, investing in a dedicated rod oven or a heater rod cabinet is a wise long-term investment.
Do not store rods in a damp locker or an unsealed tool box. If a rod coating appears cracked or flaky, it has likely been compromised by moisture and should be discarded rather than risking a structural failure on the water.
When to Weld vs. When to Call a Professional
Welding is a skill that demands practice; therefore, any repair affecting the hull’s ability to remain watertight should be scrutinized. If a crack is significant, located below the waterline, or involves structural framing, it is safer to bring in a certified marine welder.
A professional welder understands the specific regulations and metallurgy required for marine vessels. They can perform non-destructive testing, such as dye-penetrant inspections, to ensure the weld is sound and free of subsurface cracks that might remain invisible to the eye.
Use DIY welding for non-structural fittings, aesthetic repairs, or emergency “get-home” patches when no other options exist. If the boat is for offshore or heavy-water use, prioritize professional repairs over DIY fixes for all major hull damage to ensure the safety of everyone on board.
Consistent maintenance with the right materials prevents the small cracks of today from becoming the catastrophic failures of tomorrow. By understanding the metallurgy of the hull and the limitations of these welding rods, the longevity of a vessel is significantly increased. Always prioritize safety and structural integrity over convenience when performing marine repairs.
Frequently Asked Questions (FAQs)
What is the best welding rod for mild steel boat hull repairs?
The best welding rod for mild steel boat hull repairs is the E7018 low-hydrogen rod, or the E6011 rod when welding through light rust and paint. E7018 rods provide ductile, crack-resistant welds with tensile strengths around 70,000 psi, making them ideal for structural hull plating. For emergency field patches where bare metal cannot be ground clean, E6011 delivers deep penetration on AC or DCEP polarity. Always use a 3/32-inch or 1/8-inch diameter rod for typical hull thicknesses between 1/8 inch and 3/16 inch.
What does a 7018 welding rod do on a boat hull?
A 7018 welding rod produces strong, low-hydrogen welds that resist impact and fatigue cracking on structural steel boat hulls. Hull seams experience constant wave pounding and engine vibrations, which can cause brittle weld failures over time. The iron powder flux on an E7018 electrode shields the molten puddle from atmospheric moisture, keeping hydrogen levels extremely low. To maintain this protection, store opened 7018 electrodes in a rod oven held at 250 degrees Fahrenheit.
How do I prep an aluminum boat hull before using welding rods?
Prepping an aluminum boat hull requires grinding out all cracks, wiping away grease with acetone, and removing oxide with a dedicated stainless steel wire brush. Aluminum oxide melts at over 3,600 degrees Fahrenheit, whereas the aluminum hull material beneath it melts near 1,200 degrees. Failing to scrub off this transparent oxide film traps slag and causes incomplete fusion during the repair. Clean within four hours of welding with an aluminum stick rod, such as an E4043 electrode, to avoid fresh oxidation.
How do you weld a cracked boat hull below the waterline?
Repairing a cracked boat hull below the waterline involves drilling stop holes at both crack ends, beveling the seam, and welding a backing plate over the damage. Drill a 1/8-inch hole at each crack tip to stop propagation. Grind a 60-degree V-groove along the seam before applying an initial root pass using an E6010 or E6011 rod. Finish the joint with multiple stringer passes of E7018, inspect for pinholes with dye penetrant, and coat the cured joint with marine epoxy primer.
Which is better for boat hull maintenance 6011 or 7018?
Choosing between 6011 and 7018 welding rods depends on your hull surface cleanliness and joint stress requirements. E6011 electrodes penetrate deeply through dirty, rusted, or wet steel, making them superior for quick emergency repairs on older working hulls. Conversely, E7018 electrodes yield smoother, stronger welds with higher ductility and impact resistance, but they require clean, bare metal. Welds on major structural members below the waterline should always use 7018 over cleanly prepped steel.
How much do welding rods for boat hull maintenance cost per pound?
Prices for welding rods used in boat hull maintenance generally range from $3 to $15 per pound, depending on alloy type and pack size. Standard carbon steel rods like E6011 and E7018 run $3 to $6 per pound when bought in 5-pound or 10-pound containers. Specialty electrodes, such as 309L stainless steel or 4043 aluminum stick rods, typically cost $10 to $20 per pound. Buying a 1-pound repair tube costs more per pound than purchasing a 50-pound hermetically sealed tin.
Why does a welded boat hull repair crack or leak after welding?
Cracks and leaks in boat hull repairs usually occur because of trapped slag, rapid cooling, or localized stress concentrations from square patch corners. Marine repairs often fail when an operator does not chip slag between passes, creating porous channels that allow water seepage. Rapid cooling on thick steel plates hardens the bead, making it snap under hull flex. Prevent failures by grinding each pass clean, rounding repair patch edges, and leak-testing the completed repair with soapy water and compressed air.
Is it safe to weld a boat hull without removing the fuel tank?
Boat hull welding near fuel tanks requires completely draining, vapor-purging, or removing the tanks to prevent catastrophic explosions. Flammable marine fuel vapors collect in lower bilge pockets and hull cavities, where heat conduction or stray welding sparks can ignite them. Safety guidelines require disconnecting all onboard batteries, flushing tanks with soapy water, and filling fuel spaces with inert nitrogen or carbon dioxide before striking an arc. Always station an observer outside the vessel with an ABC dry-chemical fire extinguisher during hot work.

